The Benefits of Using Motorized Ball Valves in Industrial Applications
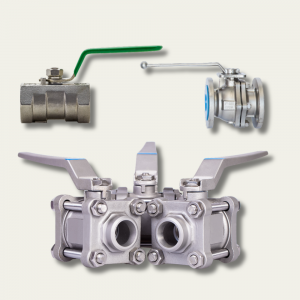
In the industrial sector, the efficiency and reliability of fluid control systems are paramount. Among the myriad of components that ensure the smooth operation of these systems, motorized ball valves stand out for their unique benefits. These valves offer enhanced control, increased safety, and improved operational efficiency, making them an integral part of many industrial applications. As industries continue to evolve, integrating advanced technologies like motorized ball valves becomes essential for maintaining competitive advantage and operational excellence.
Enhanced Control and Precision
Motorized ball valves provide unparalleled control over fluid flow, which is crucial in industries where precision is key. The automation aspect of these valves allows for:
- Precise regulation of flow rates, ensuring optimal process conditions.
- Remote operation capabilities, reducing the need for manual intervention.
- Enhanced responsiveness to changing process requirements.
The ability to fine-tune operations not only boosts efficiency but also minimizes the risk of human error. To discover expert strategies here for implementing these technologies, industries can significantly enhance their control systems.
Improved Safety and Reliability
Safety is a non-negotiable aspect of industrial operations, and motorized ball valves contribute significantly to this domain. Their design and functionality offer:
- Automatic shut-off capabilities in the event of system failures, preventing accidents.
- Reduced risk of leakage due to robust sealing mechanisms.
- Consistent performance under extreme conditions, ensuring reliable operation.
By integrating motorized ball valves, industries can bolster their safety protocols. To learn about our tailored solutions that enhance safety and reliability, these valves offer a reliable solution for mitigating risks.
Operational Efficiency and Cost Savings
Energy Efficiency
Motorized ball valves contribute to energy savings by allowing precise control and reducing unnecessary flow variations. This leads to:
- Lower energy consumption, translating to cost savings.
- Prolonged equipment lifespan due to reduced wear and tear.
- Minimized downtime, enhancing productivity.
Industries looking to optimize their energy usage can explore advanced guides and tips for integrating these valves into their systems.
Maintenance and Longevity
The robust design of motorized ball valves ensures minimal maintenance requirements. This aspect includes:
- Longer service intervals, reducing maintenance costs.
- Ease of integration with existing systems, minimizing installation time.
- Durable construction that withstands harsh industrial environments.
For industries aiming to reduce maintenance efforts and extend the lifespan of their systems, find out more about this approach to maximizing asset integrity.
Conclusion
Motorized ball valves are an invaluable asset in the industrial landscape. Their ability to enhance control, improve safety, and drive operational efficiency makes them a preferred choice across various sectors. As industries continue to prioritize sustainable and efficient operations, the role of motorized ball valves is set to become even more significant. By integrating these advanced solutions, industries can ensure they remain at the forefront of technological innovation and operational excellence. For a deeper understanding and guidance on incorporating motorized ball valves, visit Flowlink EPL’s detailed resources.
